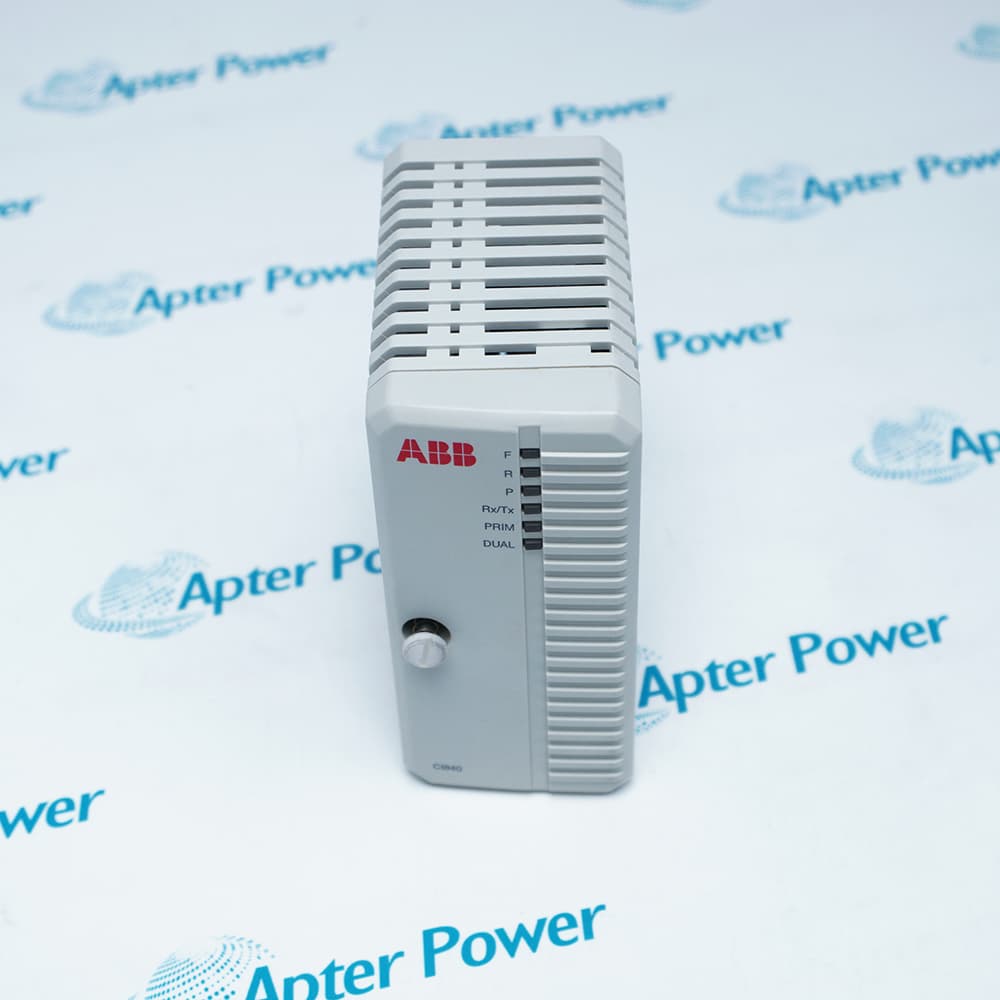
ABB NBIO-21CU
ABB NBIO-21CU
ABB NBIO-21CU
ABB NBIO-21CU
ABB NBIO-21CU
ABB NBIO-21CU
Ask our team:
  • Phone: +86 181 0690 9650
  • E-Mail sales1@apterpower.com
  • Lifecycle status

     Discontinued / Obsolete by OEM
    Apter Power guarantees premium quality ABB automation hardware, offering a fully verified source for obsolete DCS and heavy drive system replacement parts.

NBIO-21CU

/ 4.9
1001 reviews | Need a Specific Revision?
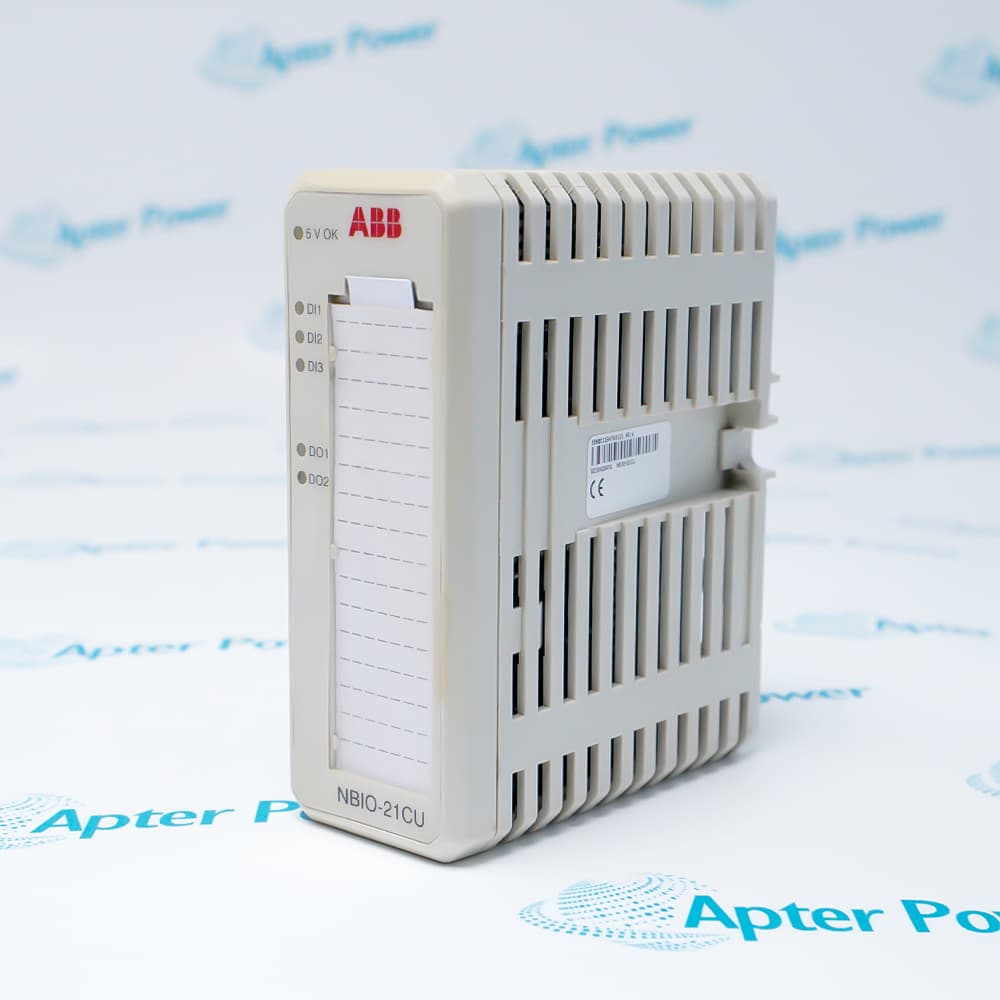
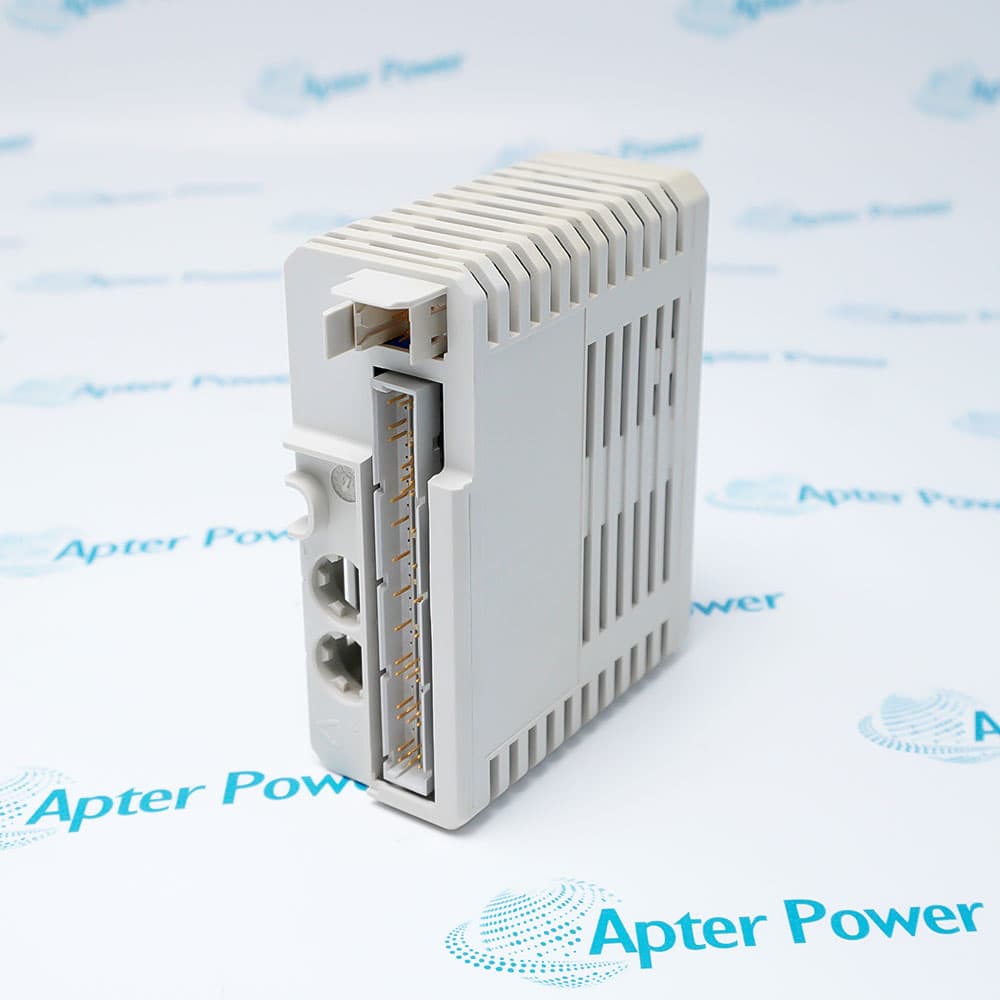
The ABB NBIO-21CU Analog I/O Unit is a analog input/output expansion board designed to establish reliable process interfaces in heavy industrial automation.
In Stock
Ships by Friday, October 30
Fast Shipping Available
Get a quick price for NBIO-21CU
Quantity
*E-mail
Company
*Mobile
*Content
Upload (gif, jpg, jpeg, png, bmp, doc, docx, xls, xlsx, ppt, pdf, csv)

Technical specifications for NBIO-21CU

  • Manufacturer:
    ABB
  • Part Number:
    NBIO-21CU
  • Product Family:
    ABB Advant OCS and Advant-800xA
  • Product Type:
    Analog I/O Unit
  • Stock:
    1
  • Power Supply:
    24 V DC
  • Input Current (max):
    50 mA
  • Output Current (max):
    500 mA
  • Operating Temperature:
    -40°C to +70°C (standard); -20°C to +70°C (certain versions)
  • Weight:
    0.5 kg
  • Estimated shipping dimensions:
    4.5 cm × 10.6 cm × 12.0 cm
  • Tariff Code:
    8537101190
  • Country of origin:
    Sweden
  • Place of shipment:
    Xiamen,Fujian,China
By purchasing this item, you agree to the Terms & Conditions, ApterPower is not an authorized distributor for listed manufacturers or tradenames and therefore the manufacturer's warranty does not apply. All our products come with ApterPower's 1-year warranty.

More Information

Overview Manuals Specifications Use Cases Communication & Connectivity Performance & Efficiency

Features:

  • Analog signal interface connecting field sensors and actuators to the S800 I/O rack backplane
  • High-precision A/D and D/A conversion capability with multi-channel configuration support
  • Designed for seamless integration with the S800 I/O series and various industrial automation platforms
The ABB NBIO-21CU operates as the Analog I/O Unit in the S800 I/O system, providing reliable analog signal processing for all modules within the control rack. It continuously converts incoming analog signals from field sensors and transmitters (including 4-20 mA current loops and standard voltage ranges) into digital data for controller processing, and generates analog output signals distributed through the rack backplane to drive actuators and field devices.

The NBIO-21CU provides essential analog I/O functions common to the entire control system, and is a critical component of the signal path, directly affecting the proper, normal operation of the overall automation system. One or multiple NBIO-21CU analog I/O units are required per rack depending on the desired channel count and signal type requirements.

For expanded analog I/O capacity applications, the S800 I/O system supports additional NBIO-21CU modules installed in supplementary rack positions. In addition to standard single module operation, the expanded configuration enables increased channel density for complex process control requirements. The S800 I/O multi-module configuration executes channel allocation using the internal addressing specified in the I/O module configuration.

The NBIO-21CU ABB Analog I/O Unit may still be available for purchase and support from Apter Power beyond End-Of-Life (EOL) by the manufacturer (OEM).
ABB NBIO-21CU Analog I/O Unit Manuals,Datasheets,Link Important Notice: Other accessories, manuals, cables, calibration data, software, etc. are not included with this equipment unless listed in the above stock item description. All prices are shown in USD.
ABB NBIO-21CU Analog I/O Unit Specs

General

  • Manufacturer ABB
  • Model NBIO-21CU
  • Condition New Original ready stock
  • Product Family NAMC-11C,NAMC-51C
Important Notice: Other accessories, manuals, cables, calibration data, software, etc. are not included with this equipment unless listed in the above stock item description. All prices are shown in USD.
  • Process Automation: Integrates with major distributed control systems like ABB Symphony Plus, Advant OCS, and Freelance 800F.
  • Drive Signal Expansion: Functions alongside industrial variable speed motor drives (such as legacy ACS 600 series) to extend control loops.
  • Field Device Regulation: Manages sensory equipment including mass flow controllers, temperature transducers, and pressure transmitters.
  • Factory Retrofitting: Acts as a reliable hot-swappable drop-in replacement part to modernize aging manufacturing assembly lines.
  • Industrial System Backplanes: Couples via fieldbus interface modules like the ABB CI854A or CI867 for system integration.
  • Noise-Immune Optical Links: Features high-speed fiber-optic data ports to exchange data cleanly without electromagnetic interference.
  • Multi-Signal Hardware Interfaces: Configured with independent channels accepting various signals (4–20 mA, 0–20 mA, and ± 10 V DC).
  • Pluggable Wiring Blocks: Implements quick-connect terminal options (such as Phoenix Contact blocks) for flexible cabling.
  • High-Precision Resolution: Offers standard 12-bit to 16-bit analog conversions to ensure sensitive tracking of process telemetry.
  • Galvanic Electrical Isolation: Incorporates robust 1.5 kV AC circuit separation to safeguard fragile control logic from harsh electrical field-side surges.
  • Low-Power Demands: Draws a lean 160 mA at 24 V DC, reducing overall cabinet thermal loading and energy footprints.
  • Rapid Signal Filtering: Implements localized hardware filtering with a response timing window of roughly 2 ms for real-time tracking.
Description
The ABB NBIO-21CU is a high-performance analog input/output unit designed for industrial automation and process control systems. This module provides comprehensive analog signal acquisition and output capabilities, enabling precise monitoring and control of physical parameters such as temperature, pressure, flow, and level in demanding industrial environments. The NBIO-21CU is specifically engineered to handle the challenges of signal conversion in complex automation architectures, receiving analog signals from sensors and transmitters and converting them into digital data for processing by control systems, while simultaneously transmitting control commands to actuators and field devices.

The NBIO-21CU addresses critical challenges in industrial signal processing by providing accurate and reliable analog-to-digital and digital-to-analog conversion. It is designed to solve the problem of signal degradation and interference that commonly occurs in harsh industrial environments, ensuring that control systems receive clean, accurate data for optimal decision-making. The module features high-precision analog conversion chips with multi-channel configuration capabilities, delivering exceptional accuracy and reliability for process control applications. Its robust design incorporates excellent anti-interference capabilities, maintaining signal integrity even in electrically noisy environments typical of manufacturing plants and processing facilities.

This versatile analog I/O unit finds extensive application across multiple industrial sectors. In the power generation and distribution industry, the NBIO-21CU is utilized for monitoring turbine parameters, generator performance, and grid synchronization signals. Chemical and petrochemical plants employ this module for precise control of reactor temperatures, pressure vessel monitoring, and flow regulation in pipeline systems. The pharmaceutical industry relies on the NBIO-21CU for batch process control, ensuring consistent product quality through accurate temperature and pressure monitoring during drug manufacturing. Food and beverage processing facilities use this unit for hygienic process control, including pasteurization temperature monitoring and filling line pressure control. Additionally, the NBIO-21CU serves critical functions in water treatment plants, oil and gas production facilities, and general manufacturing environments where reliable analog signal processing is essential for operational efficiency and safety.
Alternative Names
NBIO 21CU NBIO-21 NBI0-21CU NB1O-21CU NAMC-11C NAMC-51C NMTU-21C
Technical notes
The ABB NBIO-21CU unit acts as a critical communication bridge between physical field sensors, actuators, and the central control system, ensuring seamless signal transmission.
Exceptional Service

Our Mission

  • 100% Satisfaction

    We believe expertise is priceless. With over 20 years of experience, and top engineers on staff, we can help you solve or avoid problems that threaten your business.
  • Trust Guaranteed

    Not only do we have a vast inventory, our team makes sure every piece of equipment is in working condition. Your purchases are also backed by our Warranty.
  • Expertise

    Time is money, especially when your equipment is down. We work quickly to get your equipment on its way so you can get it back up and running.

FAQS

The following is a list of questions commonly asked by our customers. Please contact us if you have a question about our process that is not answered below.
What is the ABB NBIO-21CU designed for?
The ABB NBIO-21CU is designed to provide reliable analog and digital signal processing for industrial automation systems. It enables accurate data acquisition and signal conversion between field devices and the main control system.
What problems does the ABB NBIO-21CU solve?
The ABB NBIO-21CU helps eliminate signal degradation, communication delays, and data inconsistencies that can occur in electrically noisy industrial environments. It ensures stable and accurate signal transmission for process control.
How does the ABB NBIO-21CU improve system performance?
By supporting dedicated analog and digital I/O channels, the ABB NBIO-21CU enables fast signal processing and reliable feedback between sensors, actuators, and the host controller, improving overall control accuracy.
Can the ABB NBIO-21CU support real-time process control?
Yes. The ABB NBIO-21CU is suitable for real-time monitoring and control applications, allowing process variables to be measured continuously while simultaneously controlling connected field devices.

Product Browsing History