A Practical Bently Nevada 3500 Plan for Reducing Unplanned Factory Downtime

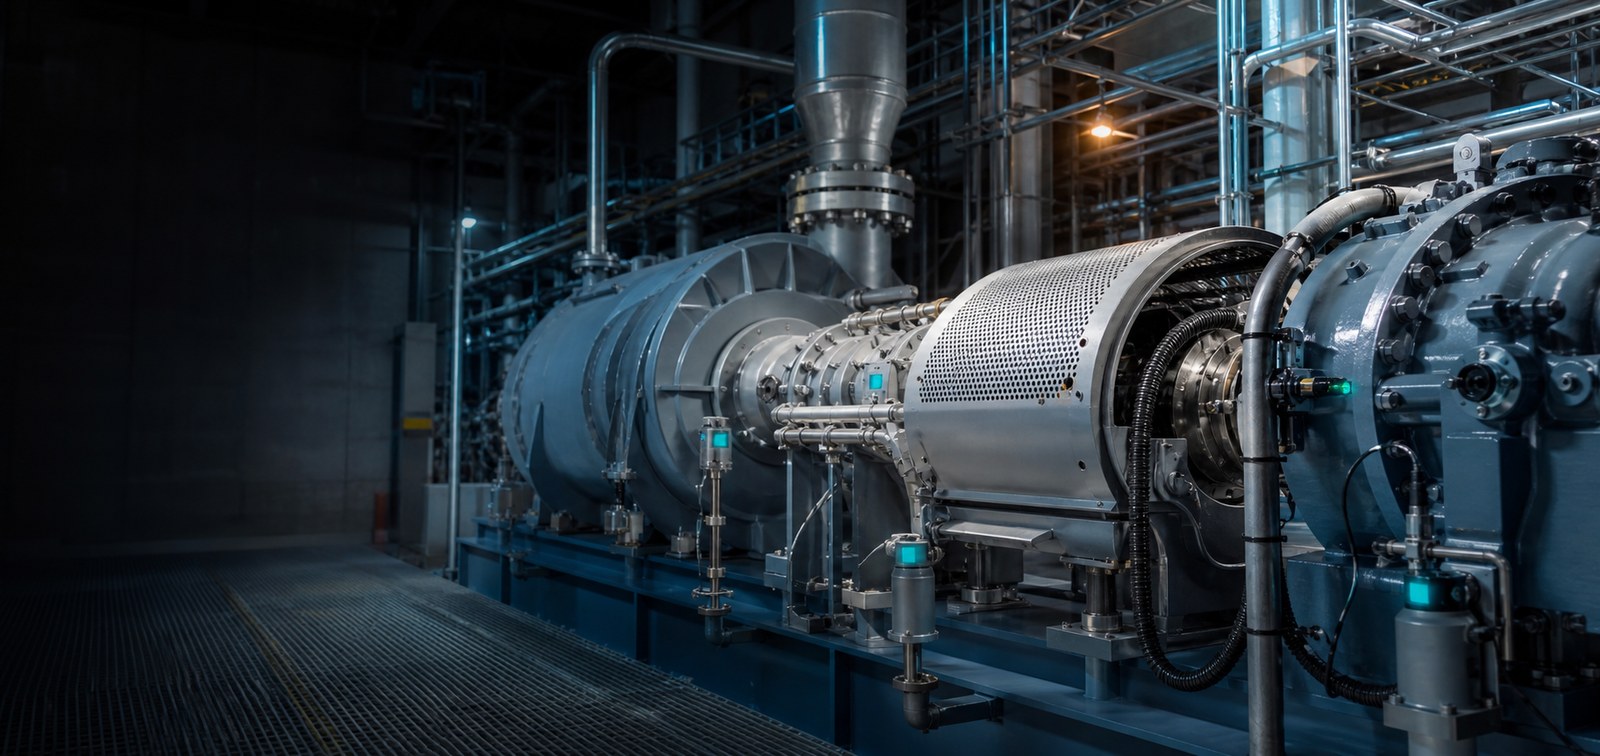
Modern rotating equipment supported by continuous condition monitoring

A practical deployment plan for moving critical rotating equipment from periodic checks and reactive repairs toward continuous condition monitoring and earlier maintenance decisions.

Factory teams responsible for compressors, pumps, turbines and fans need more than monitoring hardware. They need a clear path from field measurements to alarms, diagnostics and accountable maintenance action. This plan shows how the BENTLY NEVADA 3500 Monitoring System can support that path without making unsupported claims about guaranteed savings or downtime reduction.

The Opportunity

In modern industrial production, equipment reliability and operational safety directly affect plant productivity and economic efficiency. As factories adopt intelligent manufacturing and digital operations, condition monitoring and predictive maintenance provide an opportunity to identify developing machinery problems before they become urgent failures.

The BENTLY NEVADA 3500 Series Vibration Monitoring System, developed by GE and now associated with Baker Hughes, is widely used for continuous machinery protection and monitoring in petrochemical, power generation, metallurgy, cement and paper manufacturing environments. Its modular architecture allows a factory to build a monitoring strategy around the assets and measurements that matter most.

The Challenge

Installing a rack alone does not create a reliable monitoring program. A successful implementation must solve four connected challenges:

Measurement coverage: determine which compressors, pumps, turbines and fans are critical, then select the correct monitoring points and parameters.

Continuous protection: acquire vibration and position signals consistently, apply suitable alarm logic and make protective actions dependable.

System integration: connect field data with the control room, DCS/PLC systems and diagnostic software without creating disconnected information silos.

Operational ownership: give maintenance personnel practical alarm, trend and event information they can interpret and act on.
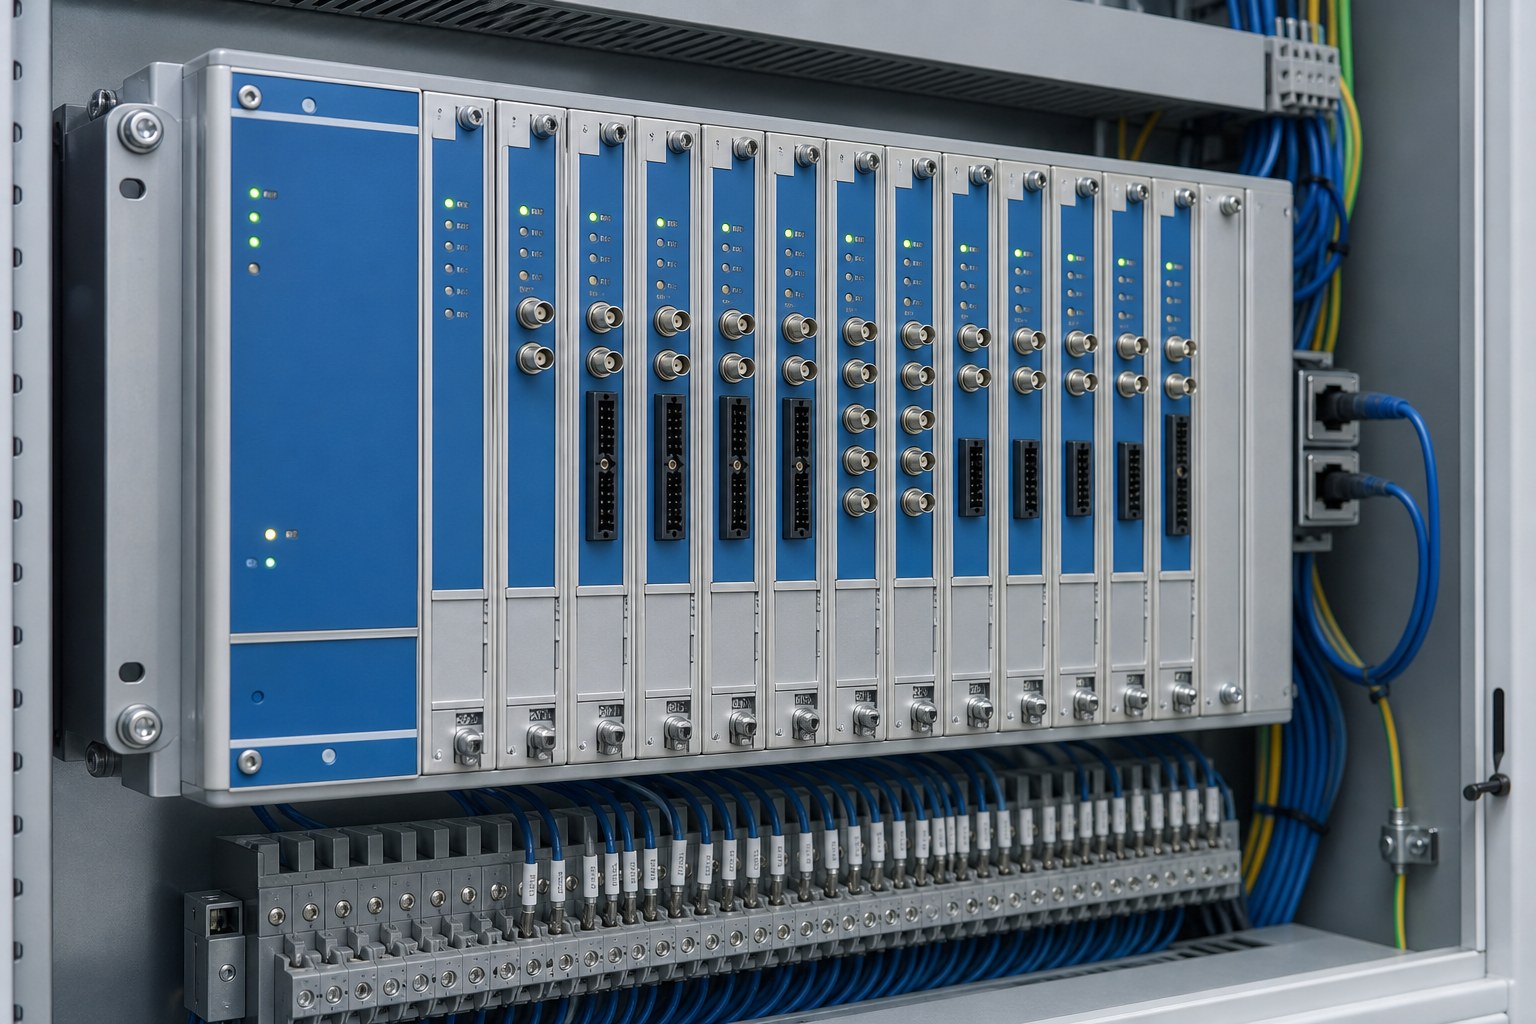
Modular machinery protection monitoring rack
Illustrative view: a modular machinery-protection rack brings monitoring, power and communication functions into one controlled cabinet architecture.

Three Core Outcomes

OUTCOME 01Earlier risk visibilityContinuous monitoring can reveal changes in shaft vibration, axial position, speed, phase, casing vibration and temperature that periodic checks may miss.
OUTCOME 02Faster maintenance decisionsAlarm records, trends and waveforms provide context for deciding whether to inspect, plan maintenance or take protective action.
OUTCOME 03A scalable foundationThe modular rack and communication interfaces allow the monitoring scope to develop with the plant.

The Solution: A Three-Layer Architecture

Layer 01

Field

3300 XL proximity probes and other selected sensors collect shaft vibration, axial position, speed, phase, casing vibration and temperature data.
→
Layer 02

Protection

The 3500 rack acquires signals, applies alarm logic and supports protective actions through the required monitoring, power and communication modules.
→
Layer 03

Management

Ethernet or Modbus/TCP connects data with DCS/PLC systems or System 1 for visualization, event review and remote diagnostics.
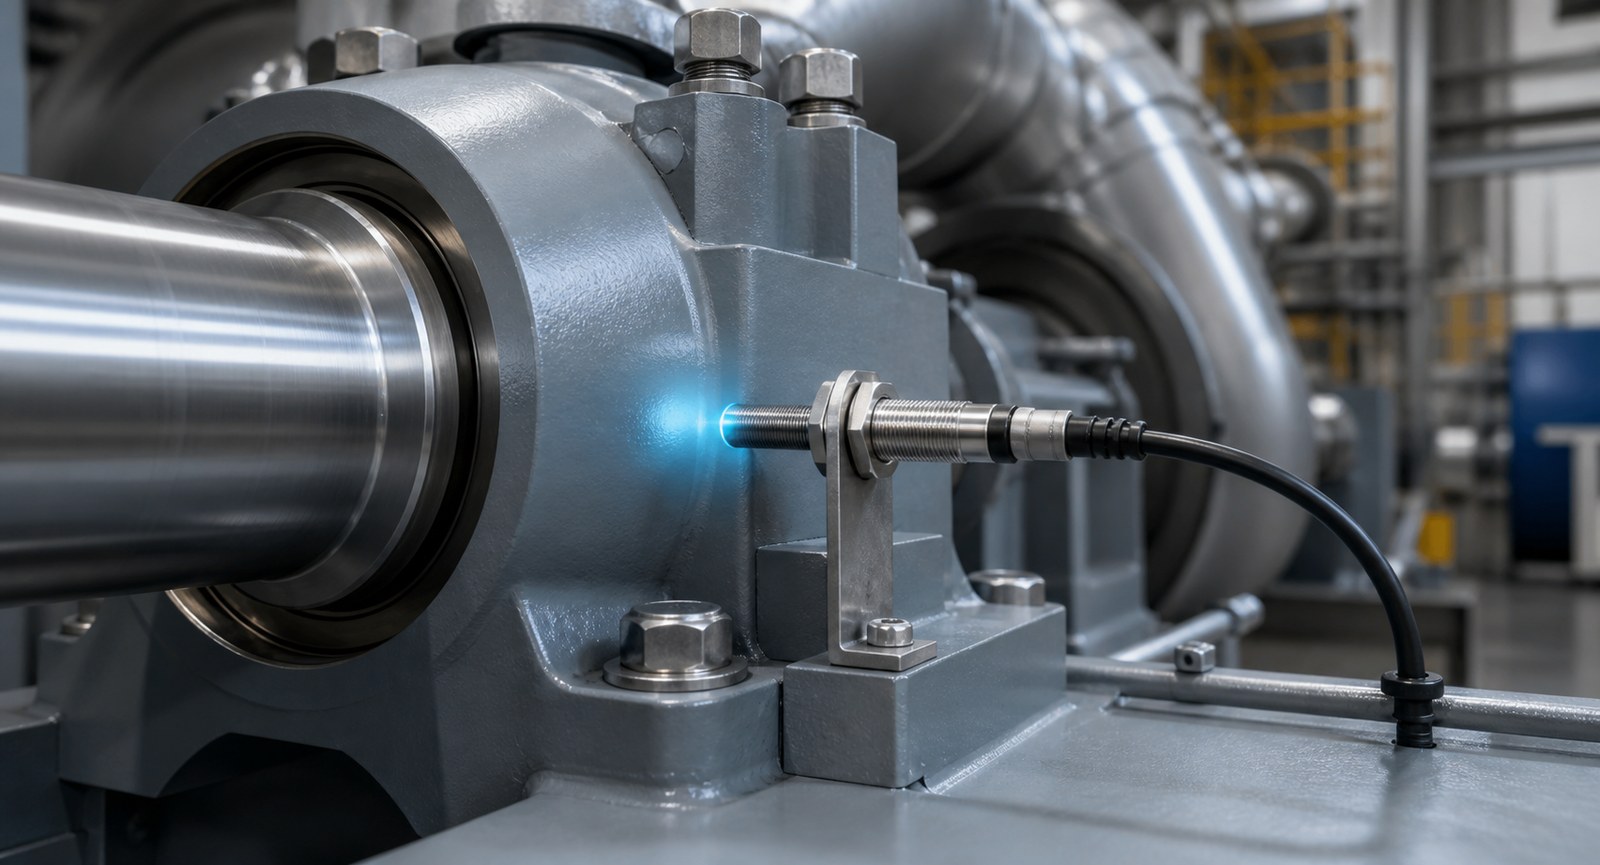
Proximity probe measurement point on rotating equipment
Illustrative view: a correctly selected and mounted proximity probe provides the field signal needed for shaft-vibration or position monitoring.

Monitoring and Diagnostic Functions

The 3500 platform uses a modular structure for multi-channel signal acquisition, real-time monitoring and alarm processing. Rack configuration should be based on the machine train, required measurements, channel count, redundancy expectations and communication requirements.

• Real-time vibration trends and waveform analysis
• Equipment health assessment and trend review
• Alarm logging and event tracking
• Diagnostic reporting for maintenance follow-up

The value is not the data alone. It is the ability to connect an abnormal signal with the affected asset, operating condition and next maintenance decision.

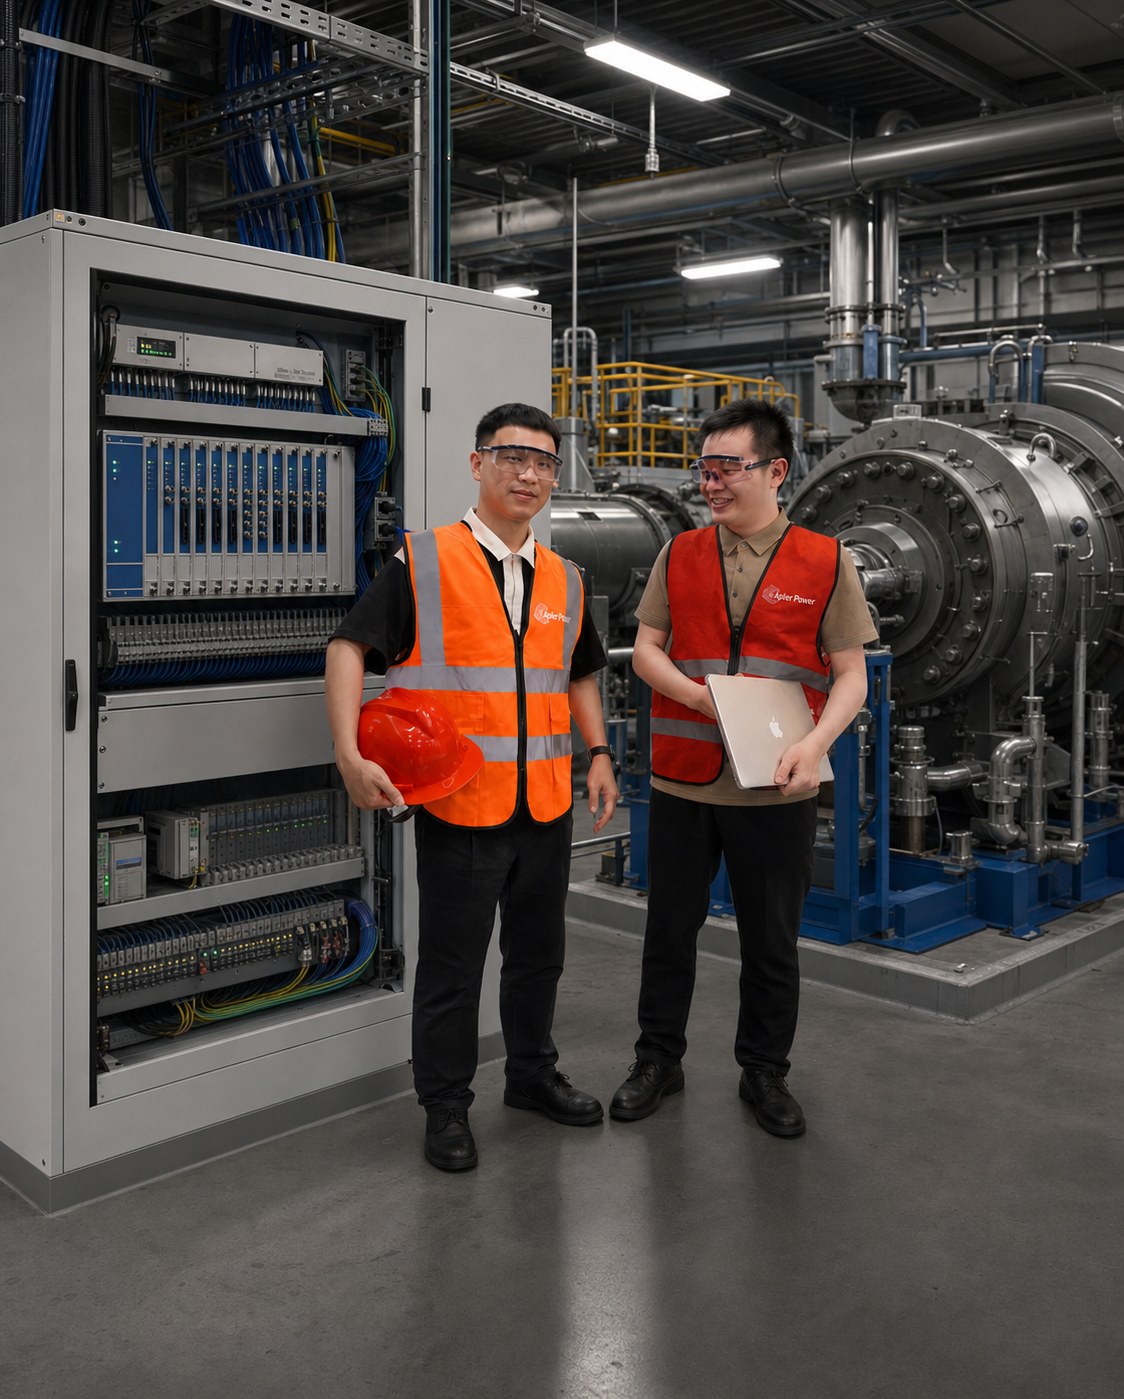
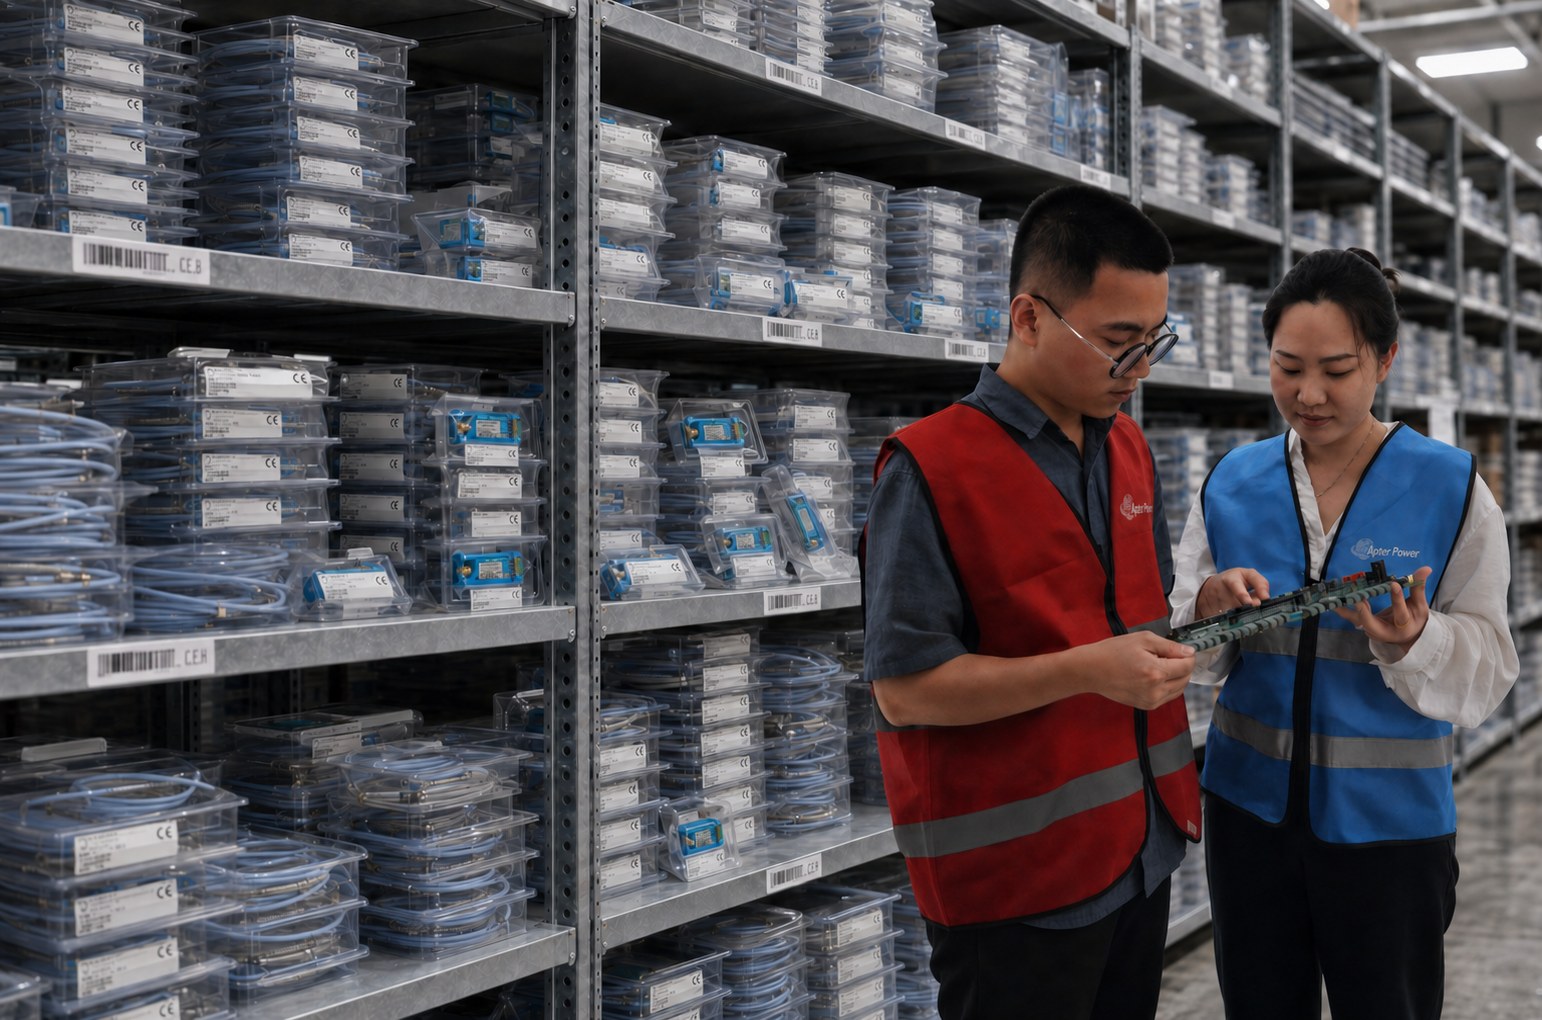
Apter Power team beside a machinery monitoring rack and rotating equipment
Apter Power team supporting a machinery-monitoring requirement.

Implementation Plan

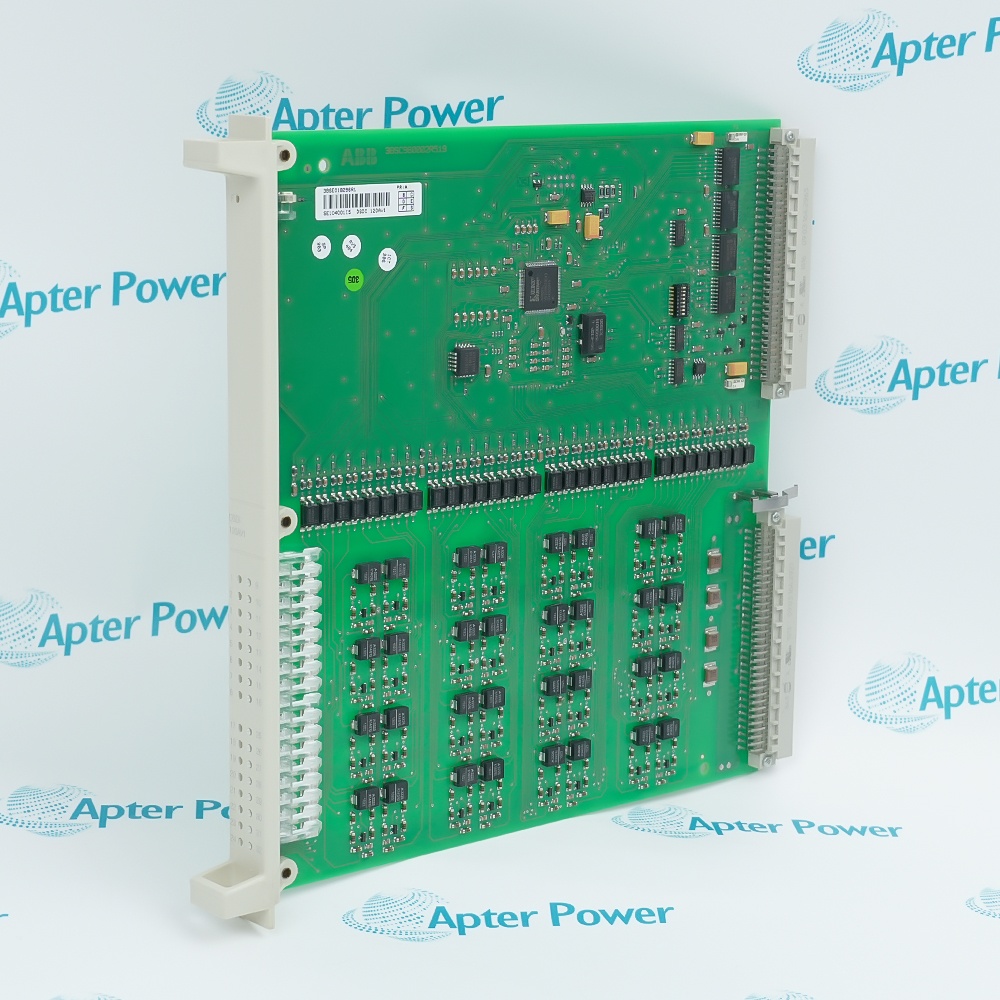
Apter Power team reviewing an industrial automation component
Apter Power team members review component details before sourcing and delivery coordination.
1

Planning

Create a critical-asset list and document measurements, channels, alarm strategy and integration points.
2

Installation & Commissioning

Confirm sensor locations, wiring, rack configuration, communication settings and alarm logic.
3

Analysis & Optimization

Establish operating baselines, review trends and refine alert thresholds using plant conditions.
4

Maintenance & Training

Define routine checks and spare requirements, then train teams to respond consistently.

The Successful Outcome

When sensors, rack configuration, communication and maintenance workflows are aligned, the factory gains continuous visibility into critical rotating equipment. Teams can identify developing conditions earlier, review evidence before taking action and plan interventions with better information. The result is a stronger foundation for reducing unplanned downtime, improving operational safety and moving from reactive maintenance toward predictive maintenance.

Actual results depend on the selected measurements, installation quality, alarm settings, machine operating conditions and the plant’s response process. These factors should be reviewed during planning rather than assumed after installation.

How Apter Power Supports the Project

Apter Power can support requirement review, component identification, availability checks, technical-document coordination and sourcing for Bently Nevada 3500 system components. Our team stays focused on the complete requirement – not only the part number – so procurement and maintenance teams have a clearer route from inquiry to delivery support.

Related Success Stories

Talk to Our Team

If your plant needs a 3500 rack, 3300 XL probes, monitoring modules, power supplies, communication interfaces or a hard-to-find replacement, send us the part number, equipment photos, quantity and required delivery date. We will review the requirement and respond with an actionable sourcing and support plan.

Request a Fast QuoteContact Apter Power

Manufacturers

Browse new, surplus and obsolete automation components from leading global manufacturers. Additional products may be available through our sourcing network.

Head Office

Apter Power | 8am-6pm ET Mon-Fri
32D GuoMao building, Hubin South Road, Siming District, Xiamen, Fujian,China
Phone+86 181 0690 9650